



When Should PLC Hardware Be Upgraded in Production?

A PLC can keep controlling a machine long after it has stopped being a sensible asset to rely on. When should PLC hardware be upgraded? Usually before an obsolete processor, failing I/O rack or unsupported communications card turns a manageable engineering job into an unplanned production stoppage. The right timing depends on risk, criticality and the condition of the wider machine - not simply the age shown on the panel door.
For a production site, a PLC upgrade is about more than replacing a controller. It is an opportunity to protect uptime, improve fault finding and make sure the machinery remains safe, supportable and capable of meeting the demands placed on it.
When should PLC hardware be upgraded?
The clearest trigger is obsolescence. If a PLC manufacturer has discontinued a processor, power supply, I/O module or programming software, the equipment may still work perfectly well today. The issue is what happens at 2 am when a module fails and no approved replacement is available from stock.
A discontinued platform creates several operational risks. Spare parts may be expensive, used or unverified. Programming software may only run on an ageing laptop. Engineers may need specialist knowledge that is increasingly difficult to source. A simple electrical fault can then lead to extended downtime while parts are located, code is recovered or a temporary workaround is built.
This does not mean every older PLC needs immediate replacement. A low-risk standalone unit with a proven spare held on site may be suitable for continued service. A controller running a critical conveyor, carton erector, filling line or safety-related process deserves a different decision. The upgrade priority should reflect the consequence of failure, not a blanket age limit.
Signs that the risk has become unacceptable
Repeated nuisance faults, intermittent I/O losses, processor memory warnings and unstable communications all deserve investigation. They may be caused by wiring, power quality, sensor issues or network faults rather than the PLC itself. But if the hardware is difficult to diagnose or replace, recurring faults are a strong reason to plan an upgrade.
Other warning signs include a growing dependence on obsolete HMIs, serial communications that limit integration, unavailable software licences, or a control panel with no realistic space for safe maintenance. If only one person understands the machine code, the business also has a resilience problem. Good hardware cannot compensate for undocumented logic and an inaccessible programme backup.
A particularly urgent case is where safety, compliance or cybersecurity is compromised. Older PLCs are not automatically unsafe, and not every system needs to be networked. However, a controller that cannot support required safeguarding changes, secure access arrangements or traceability expectations should be reviewed promptly by competent engineers.
Upgrade before failure becomes the project plan
Reactive replacement is sometimes unavoidable, especially after a catastrophic breakdown. It is rarely the best route. Emergency work usually means limited time to survey the system, uncertain availability of components and little opportunity for proper testing. Production pressure can also force decisions that leave temporary arrangements in place for too long.
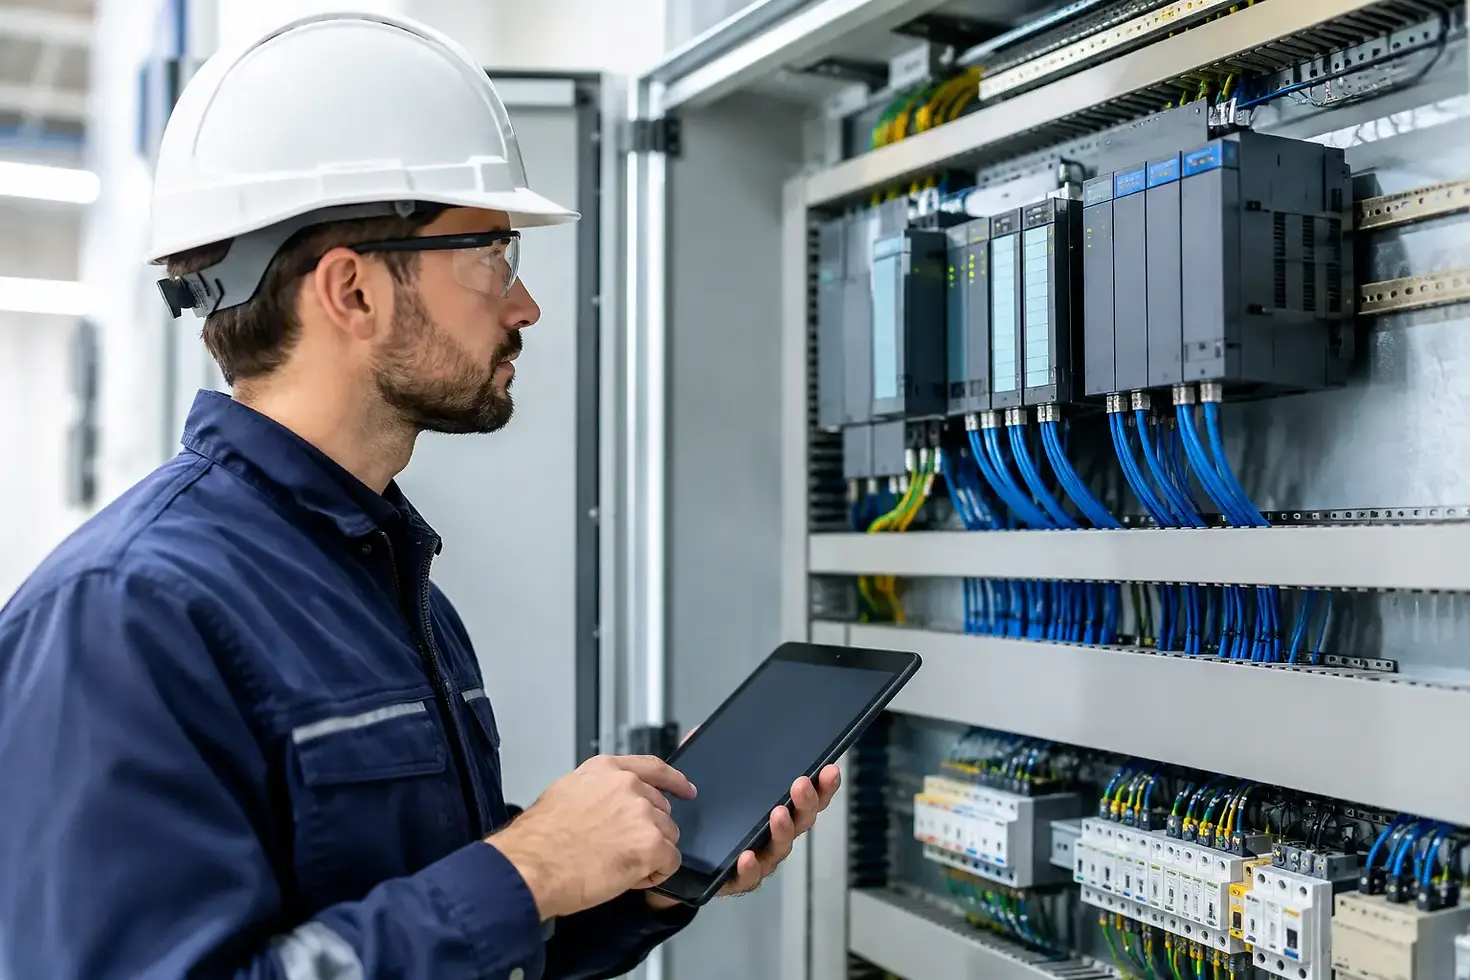
A planned PLC hardware upgrade gives the site control. Engineers can assess the existing electrical drawings, PLC programme, I/O allocation, field devices, drives, safety circuits and operator interface before selecting a replacement platform. The work can then be aligned with a shutdown, a product changeover or a quieter production period.
The commercial case should include more than the purchase price of the new PLC. Consider the likely cost of lost output, missed customer deliveries, overtime, emergency call-outs and the time required to recover a line after a major control failure. In many cases, a controlled upgrade costs less than one prolonged breakdown on a bottleneck asset.
Do not judge the PLC in isolation
Replacing a processor alone may not remove the real risk. The existing power supply, remote I/O, network switches, analogue modules, motion equipment and HMI may be equally obsolete. Conversely, a full panel replacement may be unnecessary if the panel is sound, documentation is accurate and only the CPU platform has reached end of life.
A practical survey establishes the scope. It should identify every component that is no longer supported, assess the condition of the cabinet and wiring, and check whether the existing programme can be uploaded and validated. It should also confirm whether the new PLC can communicate with drives, scanners, weighing systems, printers and other machine equipment without introducing avoidable complexity.
This is where real-world expertise matters. A like-for-like migration can reduce commissioning time, but it may preserve poor logic, unclear alarms and historic modifications. A wider modernisation can improve diagnostics and performance, but it brings more testing, more change control and a larger initial investment. The best option is the one that reduces operational risk without creating unnecessary disruption.
Prioritise the assets that can hurt production most
For sites with several legacy systems, attempting to upgrade everything at once can be disruptive and difficult to manage. Build a prioritised register instead. Rank each PLC-controlled asset by production criticality, hardware availability, fault history, safety exposure, programme backup status and the availability of engineers who can support it.
The highest priorities are normally bottleneck machines, equipment with no practical manual fallback and systems where a fault can stop an entire process area. A failed PLC on a single ancillary machine may be inconvenient. A failed controller on a main conveyor system can halt packing, despatch and customer deliveries within minutes.
It is also sensible to review commonality. Standardising selected PLC platforms across a plant can simplify spares holdings, programming access and engineer training. Standardisation should not be pursued blindly, though. A platform that suits a straightforward conveyor application may not be appropriate for a high-speed motion machine or a complex process skid.
What a controlled PLC upgrade should include
A successful project begins with information, not hardware. Before work starts, capture current electrical drawings, panel layouts, programme files, drive parameters, HMI screens and network settings. Where documentation is missing, allow time to verify the system on site. Assumptions made during a rushed migration often appear later as commissioning delays.
The replacement solution should be designed around maintainability. Clear terminal labelling, sensible I/O grouping, documented network addresses and readable alarm messages make future fault finding quicker. The programme should be backed up in a controlled location, with the software version and access arrangements recorded for the engineering team.
Testing needs to be proportionate to the machine but never treated as an afterthought. Off-line code review and bench testing can reduce risk before shutdown. On site, the work should include I/O checks, interlock verification, safe start-up checks, functional testing and monitored production trials. Any changes to safety functions require the appropriate assessment, validation and records.
Commissioning plans should also include a rollback position where practical. Keeping the old controller and a verified backup available during the early stages can protect the production schedule if an unexpected issue arises. Once the line is stable, update drawings, hand over backups and make sure the maintenance team understands the revised system.
Avoid waiting for the perfect moment
There is rarely a completely convenient time to take a production asset out of service. That is why PLC upgrades are often delayed until a failure makes the decision for the business. The better approach is to use fault trends, obsolescence notices and production criticality to create a rolling upgrade plan.
Start with an honest assessment of the equipment most likely to cause costly disruption. Put spares and programme backups in place for systems that cannot yet be upgraded, then schedule the highest-risk work around the operation. A capable engineering partner can support the survey, migration, commissioning and aftercare, while keeping the focus where it belongs: safe, reliable production.
MechElecPro Solutions takes this partnership-driven approach because a PLC upgrade should leave your team with a machine that is easier to support, not simply a newer controller in the cabinet. Acting while the line is still running gives you time to make sound decisions, test properly and keep your operation moving.


Comments